Cannabis & Hemp Extraction Equipment
The Prodigy crude-to-API pipeline brings together ProX closed-loop hydrocarbon extraction, MPS post-processing, inTEST thermal management, GC active solvent recovery, and custom builds for cannabis and hemp operations. Pharmaceutical-grade construction and GMP documentation connect the complete production line. Full GMP documentation and the IQ/OQ/PQ validation package are available for all Prodigy systems.
ProX
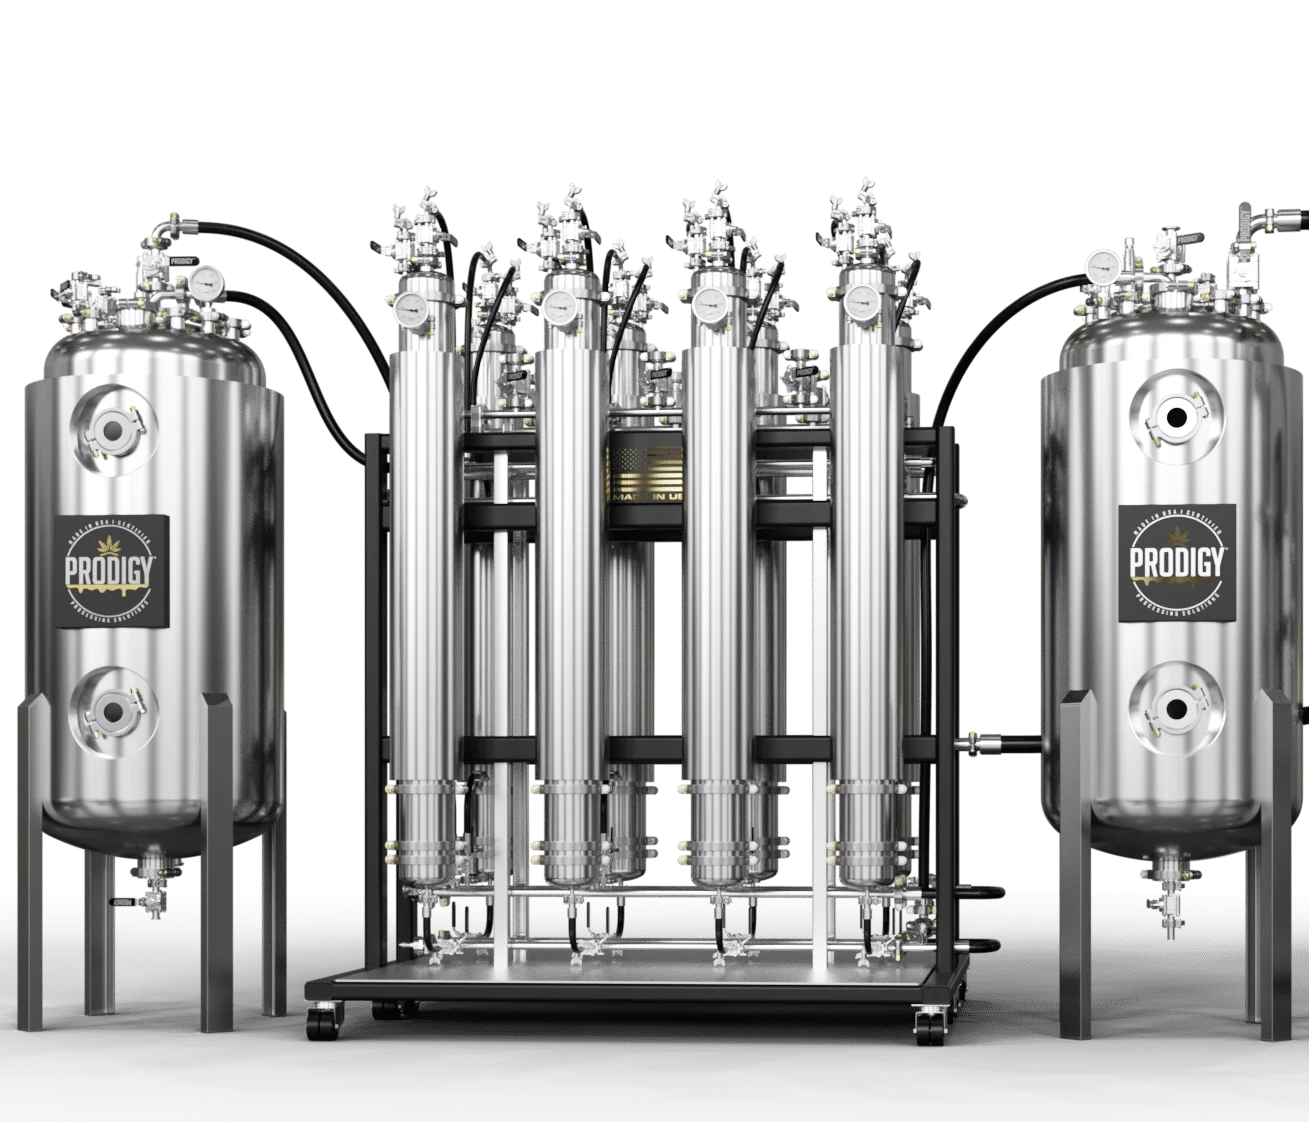
Pharmaceutical-Grade Hydrocarbon Extraction System
From crude biomass to pharmaceutical-grade extract — in a single, validated, closed-loop system.
The ProX is Prodigy's flagship hydrocarbon extraction platform, engineered from the ground up for pharmaceutical-grade cannabinoid crude production. Built to ASME BPE-2024 standards with 316L pharmaceutical-grade stainless steel product-contact surfaces, the ProX is the foundation of the Prodigy crude-to-API pipeline.
Designed for seamless tandem operation with the MPS Multi-Processing System, the ProX delivers consistent, reproducible crude extract with the documentation and validation infrastructure required for FDA cGMP and EU GMP compliance.
ProX delivers faster, more efficient extraction with industry-leading low solvent loss, rapid solvent recovery, pharmaceutical-grade weld quality, and integrated documentation designed to support compliance and operational confidence.
Key Features
- Closed-loop hydrocarbon extraction with full solvent recovery
- 316L pharmaceutical-grade stainless steel product-contact surfaces
- C1D1-rated electrical components for hazardous location compliance
- Piped in tandem with MPS for continuous batch production
- ASME BPE-2024 fabrication for pharmaceutical and bioprocessing applications
- GMP documentation, cleaning validation, and SOPs
- Scalable configurations for pilot, clinical, and commercial production
- Full GMP documentation and IQ/OQ/PQ validation package available
MPS 30
Multi-Processing System — THCa, HTE & Distillate Refining
Three output capabilities. One integrated cannabis post-processing platform.
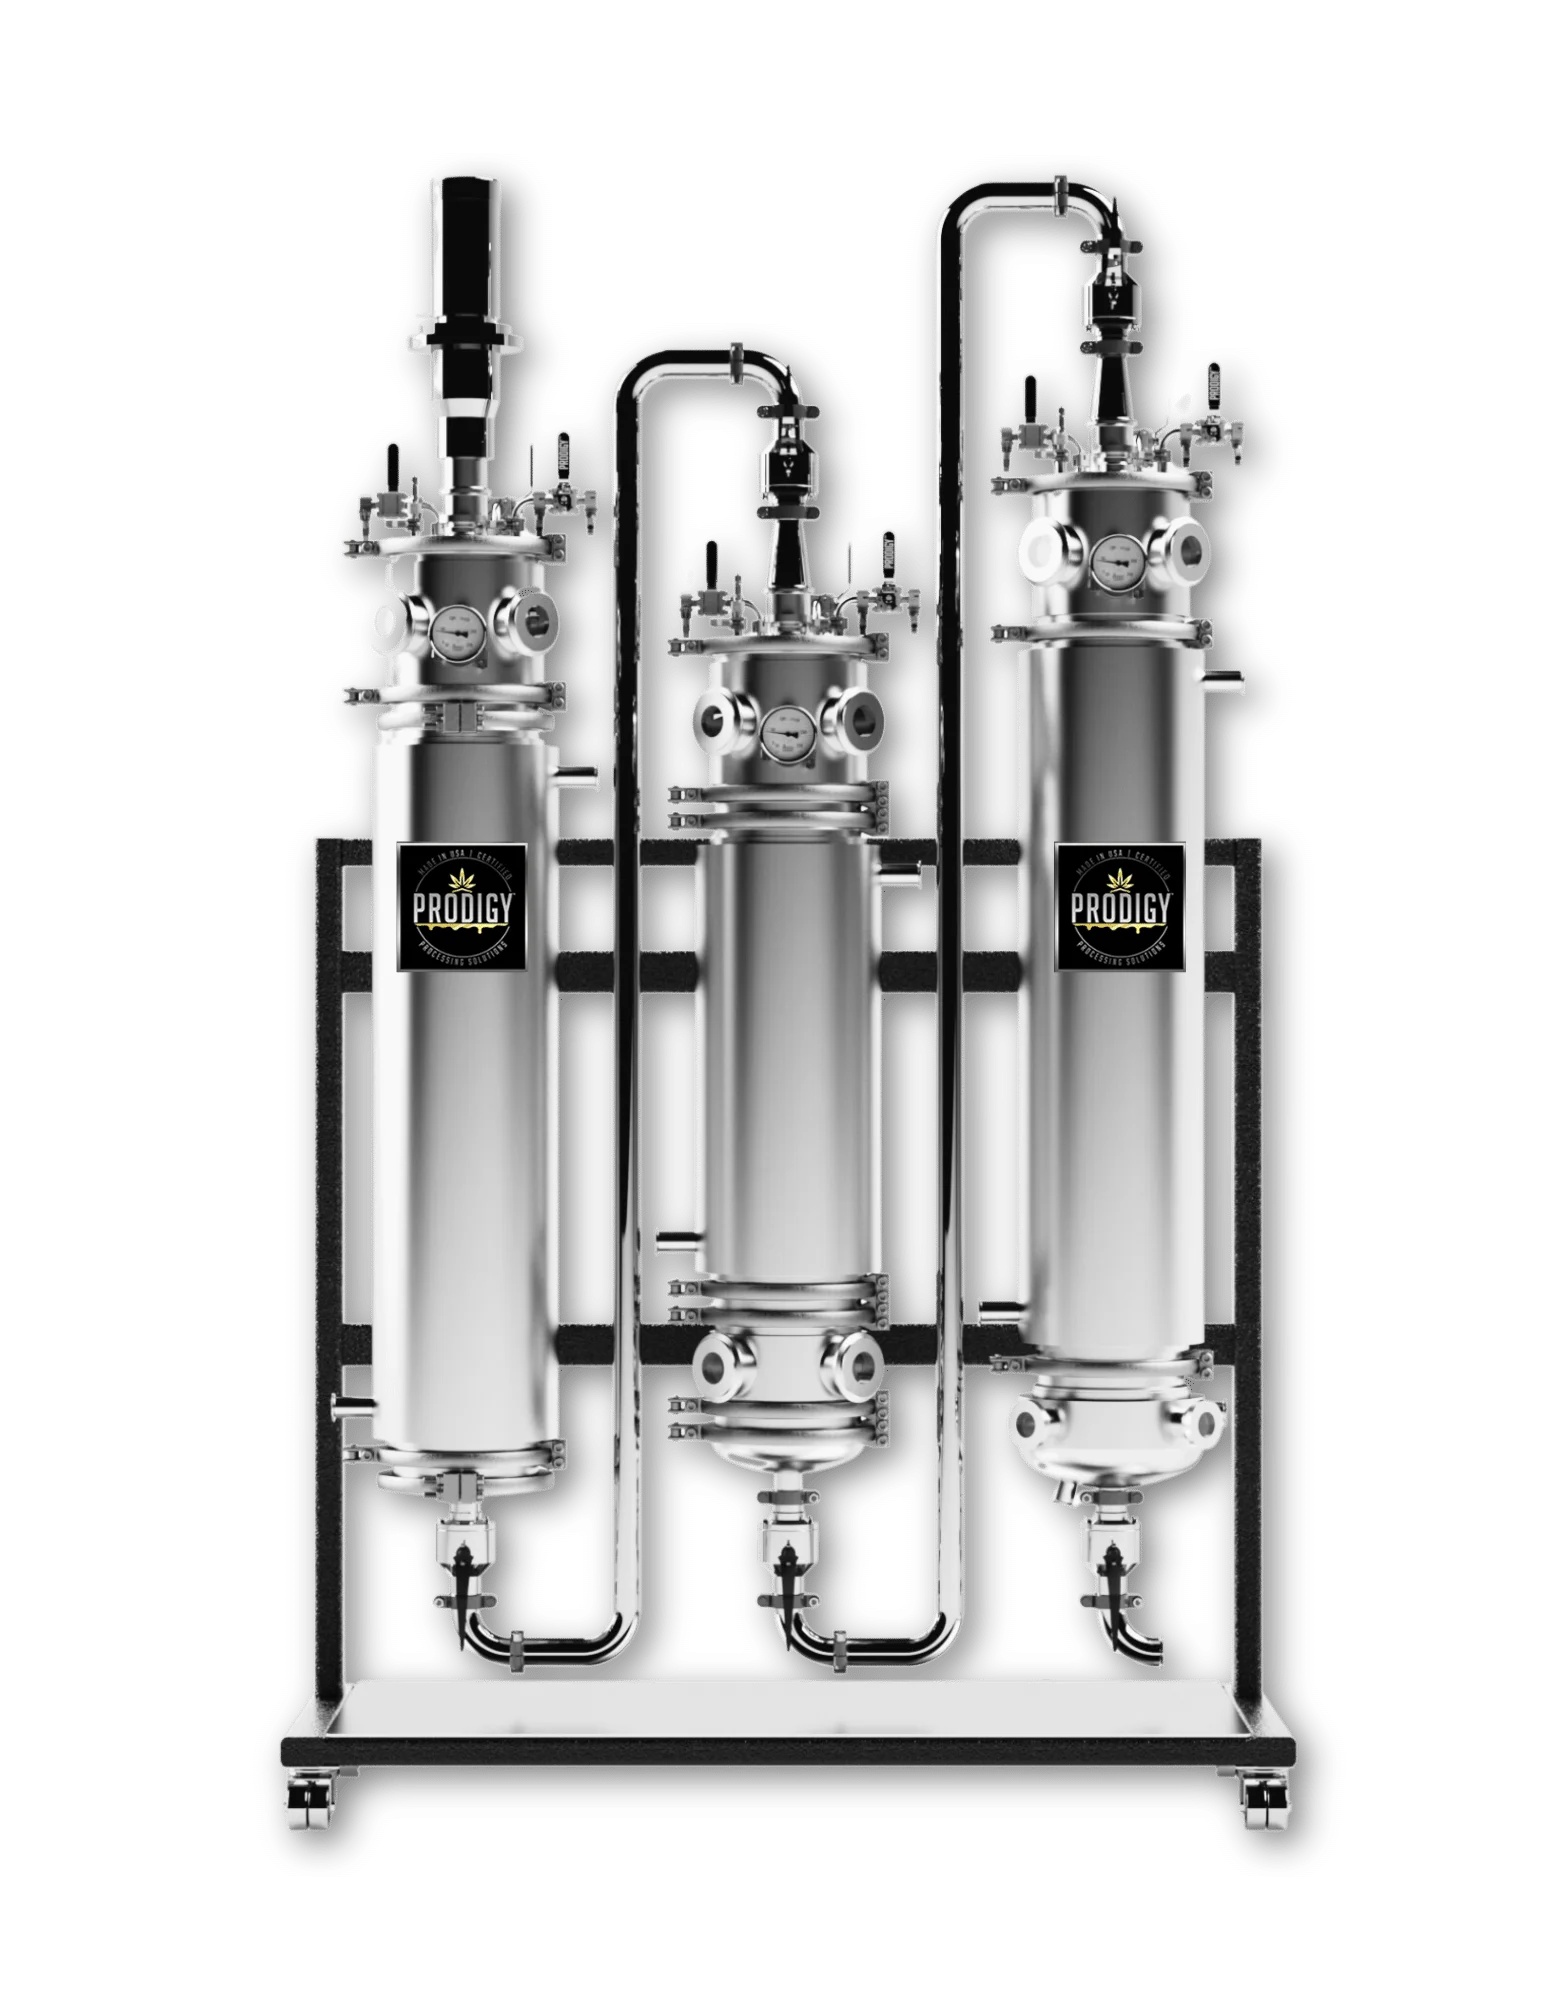
The MPS 30 combines THCa isolation, filtration, High Terpene Extract (HTE) separation, and cannabinoid distillate refining in an integrated three-vessel platform. Testing demonstrated refinement of crude or decarboxylated cannabis extract into high-purity concentrated cannabinoid distillate without a separate wiped-film or short-path system.
The MPS also produces ~99%+ pure cannabis isolate (e.g., THCA). Its three 30L jacketed vessels use 316L pharmaceutical-grade stainless steel, with ASME BPE fabrication and inline decarboxylation, solvent purge, and degassing configurations available.
The MPS streamlines post-processing with an integrated inline workflow that reduces material handling, maintains a closed processing environment, and minimizes contamination risk for cleaner, more consistent production.
Key Features
- Integrated platform for THCa isolation, filtration, HTE separation, and distillate refining
- Demonstrated crude or decarboxylated extract-to-distillate refining without separate WFE/SPD equipment
- 30L jacketed isolation vessel with pneumatic or C1D1-rated agitation
- Detachable 316L stainless steel yield filter basket with 25-micron filtration
- 30L filtration vessel with centered sintered disc filtration and optional media treatment
- 30L HTE collection/evaporation vessel with fan-head injection for terpene capture
- Configurable for inline decarboxylation, solvent purge, and degassing
- Piped in tandem with ProX for continuous batch production
- ASME BPE-2024 fabrication for pharmaceutical and bioprocessing applications
- GMP documentation, cleaning validation, and quality-control programs
- Scalable for cannabis, hemp, pharmaceutical R&D, and commercial API production
inTEST
Precision Thermal Management — Industrial Chillers
Precise, reliable temperature control for pharmaceutical extraction and post-processing environments.
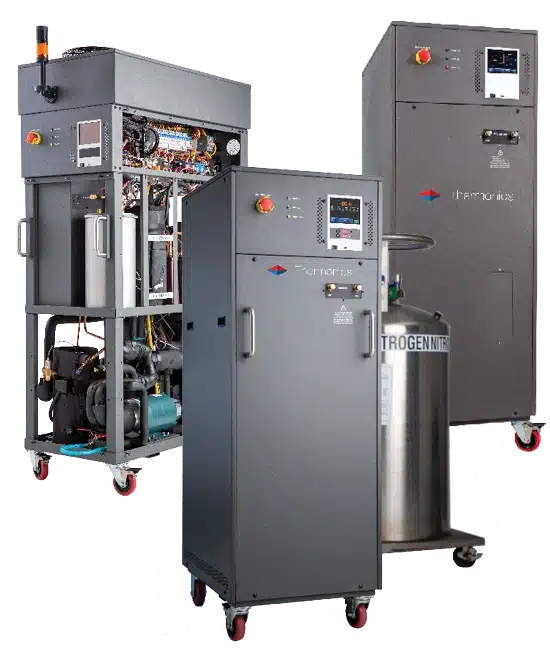
The inTEST chilling systems provide the precise thermal management required for pharmaceutical-grade cannabinoid extraction and post-processing. Engineered for compatibility with the ProX and MPS systems, inTEST units deliver consistent, validated temperature control across cryogenic and heated jacket applications.
Built for pharmaceutical and industrial environments, inTEST systems are designed with redundant safety systems, pharmaceutical-grade construction materials, and the documentation infrastructure required for GMP validation.
Why Prodigy selected inTEST: Purpose-built for pharmaceutical and industrial thermal management with the precision, reliability, and documentation infrastructure that extraction environments demand. Unlike general-purpose chillers, inTEST units are engineered for the exact temperature profiles and duty cycles required by hydrocarbon extraction and crystallization processes.
Key Features
- Precise temperature control for cryogenic and heated jacket applications
- Redundant safety systems for pharmaceutical environment reliability
- Designed for seamless integration with ProX and MPS systems
- Pharmaceutical-grade construction materials
- GMP validation documentation package available
- Scalable cooling capacity for pilot to commercial production
In Stock · Ready to Ship
PROCHILL™ LC-5.000.170 Process Chiller
5 kW of cooling at −80°C and 11 kW at −60°C from one unit. Explore its −80°C to +25°C operating range, programmable fluid-pressure control and remote-control capabilities.
Subject to prior sale. Confirm current stock and unit-specific installation requirements.
Custom Builds
ASME BPE Custom Engineering — Any Scale, Any Application
Bespoke pharmaceutical-grade processing systems engineered to your exact specifications.
Prodigy's custom engineering capability delivers bespoke pharmaceutical-grade processing systems for applications that require more than an off-the-shelf solution. From pilot-scale R&D systems to commercial API manufacturing lines, every custom build is engineered to ASME BPE-2024 standards with full pharmaceutical documentation.
Custom builds are available in any configuration, scale, or material specification required by your application. All custom systems are manufactured by Mitchell Fabricators in Hartville, Ohio. Full GMP documentation and the IQ/OQ/PQ validation package are available for FDA cGMP, EU GMP, and international regulatory projects.
Key Features
- Engineered to ASME BPE-2024 for pharmaceutical and bioprocessing applications
- Any scale: pilot production through commercial API manufacturing
- 316L pharmaceutical-grade stainless steel standard; other alloys available
- Full compliance pathway: FDA cGMP, EU GMP EudraLex Vol. 4, ICH Q7
- CRN, CE/PED, and hazardous-location electrical configurations available
- Full GMP documentation and IQ/OQ/PQ validation package available
- GMP SOPs, cleaning validation, and change control documentation
- Manufactured by Mitchell Fabricators — ASME-certified fabrication partner
GC Series
Oil-Free C1D1 LPG Gas Compressors for Active Solvent Recovery
Supercharge your solvent recovery — up to 4-10x faster than passive operation.
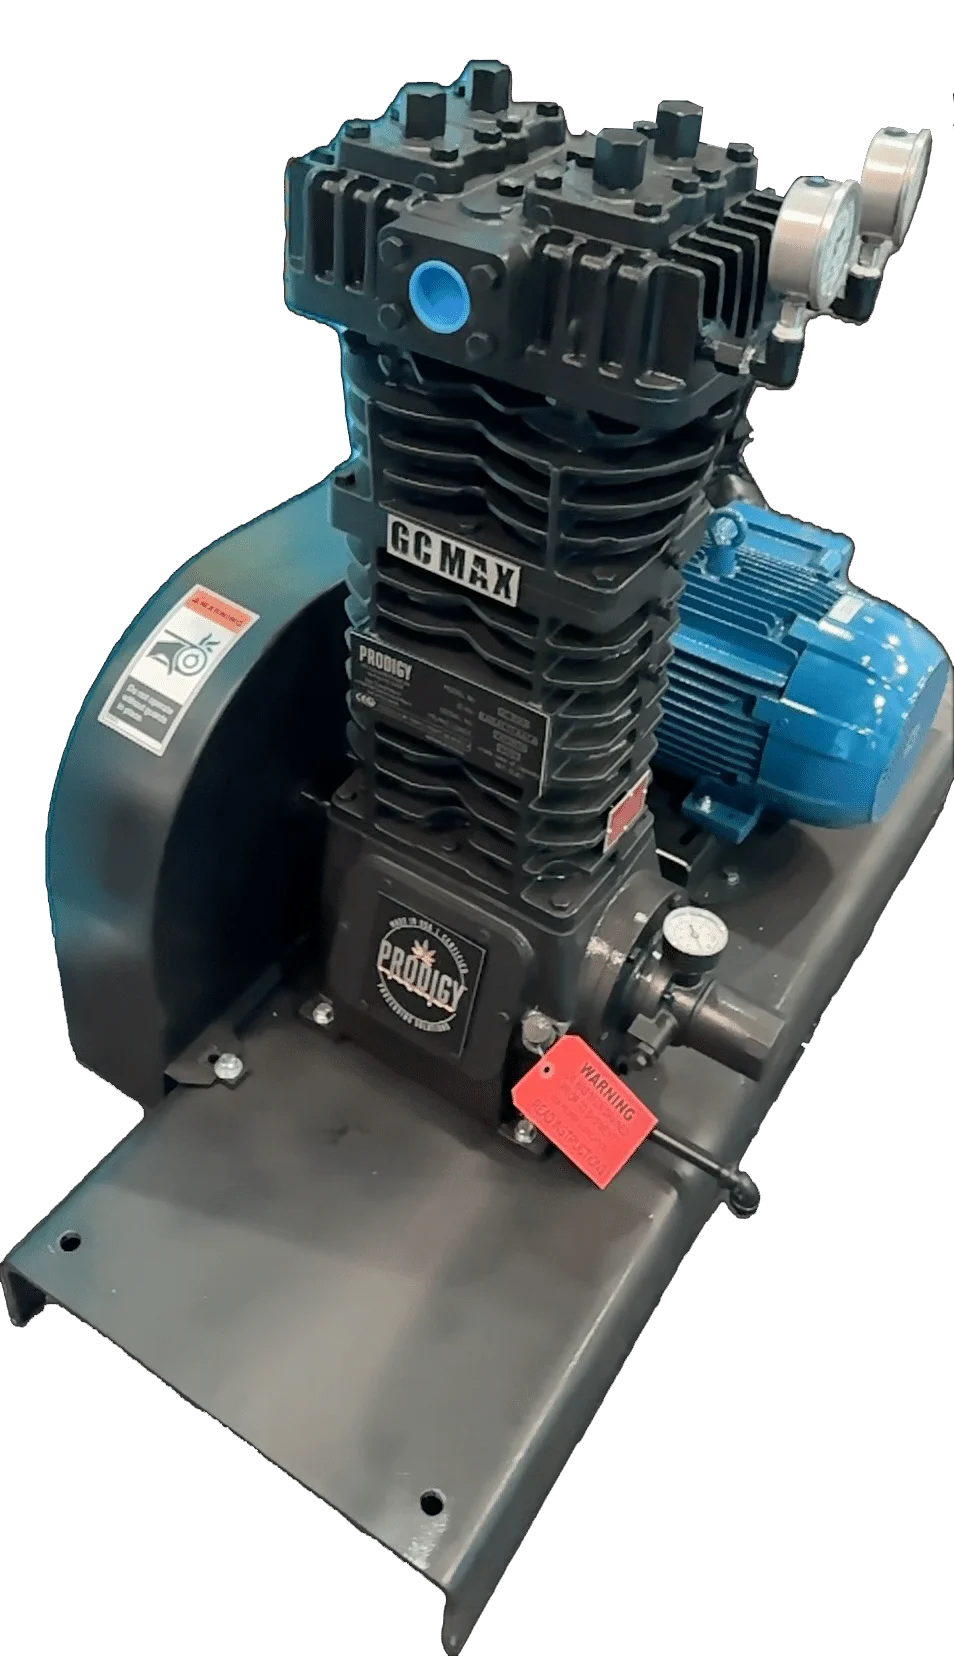
Prodigy's GC Series oil-free reciprocating gas compressors are purpose-built for active solvent recovery in LPG, butane, and propane cannabis extraction. Active recovery systems dramatically accelerate the extraction cycle while improving solvent recovery efficiency, reducing waste, and lowering operating costs.
All GC Series compressors feature ductile iron heads and cylinders, high-efficiency valves, steel pistons, and self-adjusting piston rod seals designed for quiet, efficient handling of propane, butane, and anhydrous ammonia. Available in three configurations — GC LUX, GC PRO, and GC MAX — to match any production scale.
The GC Series delivers the fastest active solvent recovery in the industry with oil-free operation, C1D1 compliance, and robust construction rated for continuous commercial use.
Key Features
- Active solvent recovery — up to 4-10x faster than passive operation*
- Oil-free compression with PTFE seals for clean solvent recovery
- C1D1 compliant for Type 6 & Type 7 licensed facilities
- UL Listed, ISO 9001, ATEX Certified*
- Canadian CRN & European Union CE ready*
- Ductile iron head and cylinders for sustained high-level performance
- Self-adjusting piston rod seals for low maintenance
Choose Your Model
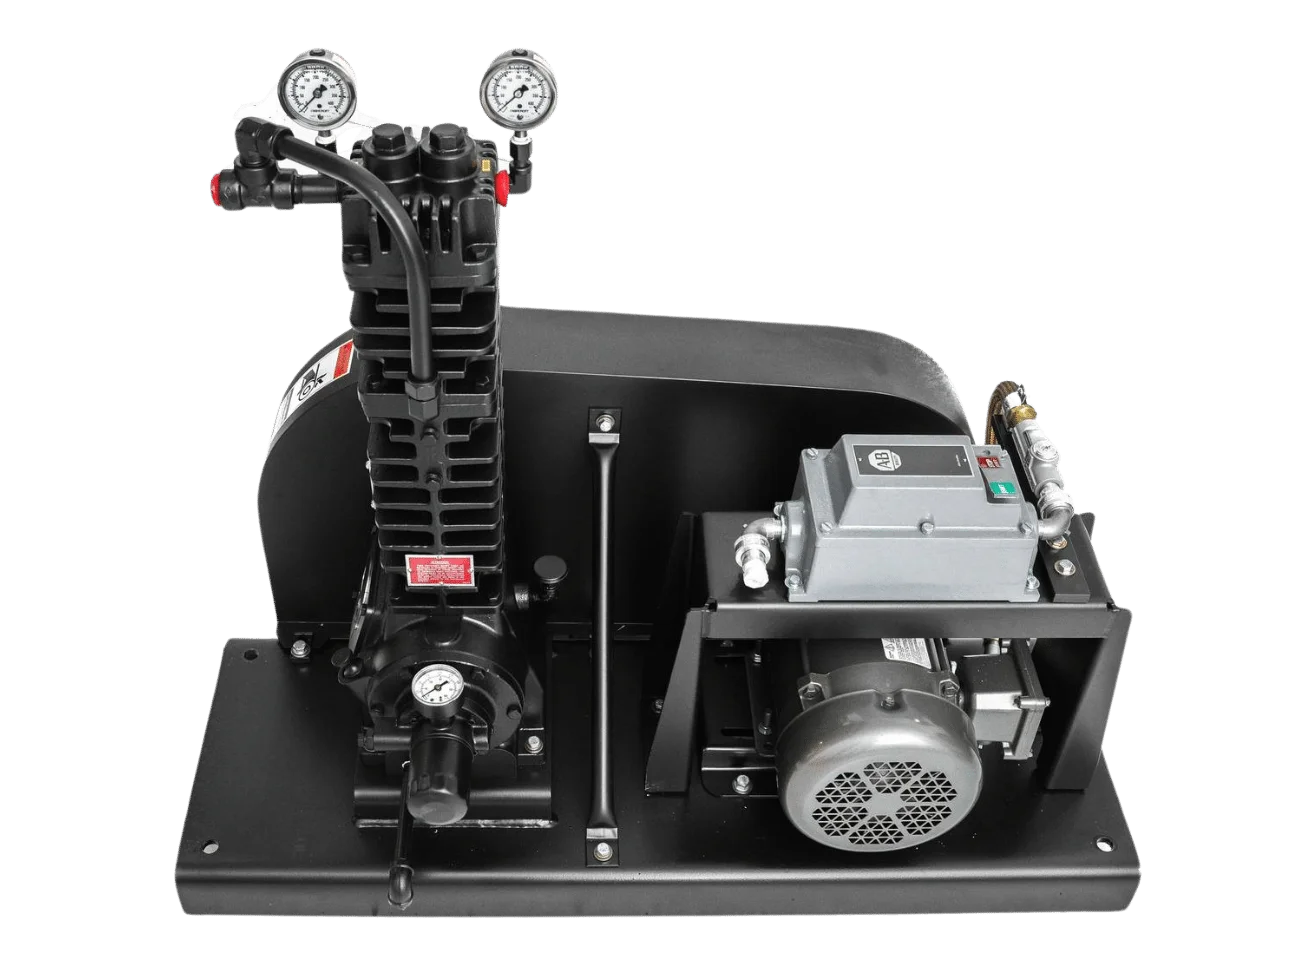
GC LUX
Single-cylinder oil-free reciprocating gas compressor for smaller extraction operations.
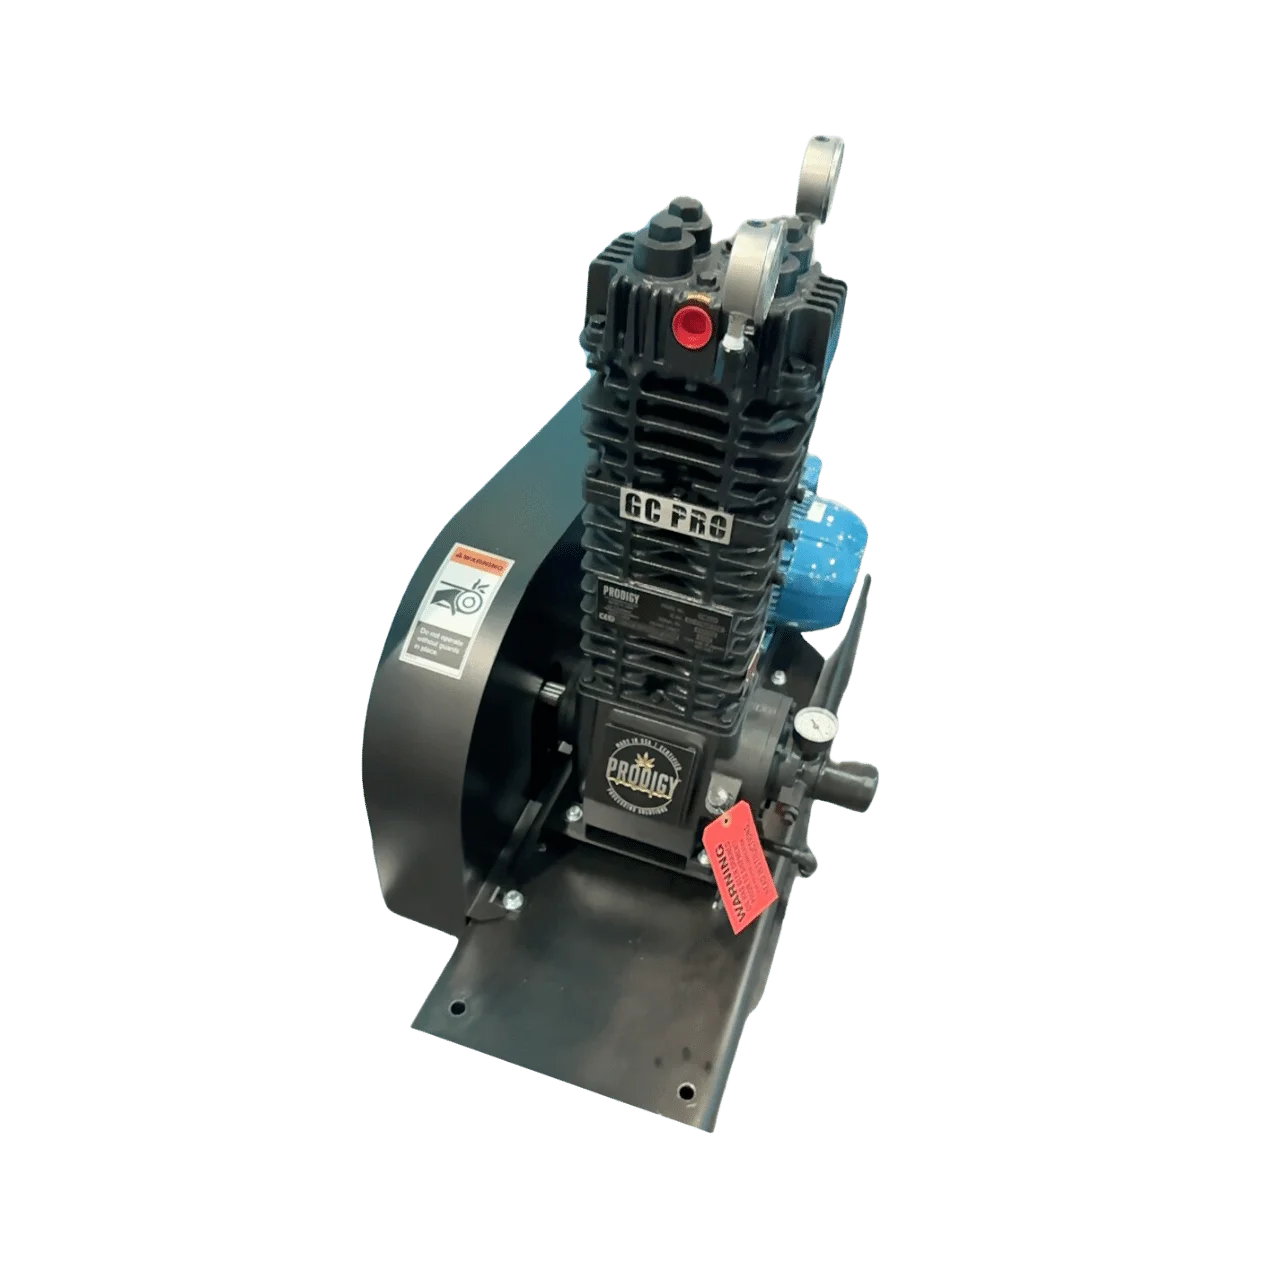
GC PRO
Mid-range two-cylinder oil-free reciprocating gas compressor for growing operations.
GC MAX
High-performance two-cylinder compressor for large-scale commercial extraction.
All models: 350 PSIA MAWP · 350–825 rpm · Oil-free piston, PTFE seals · Ductile iron head & cylinders*
Ready to Configure Your System?
Every Prodigy system is configured to your specific application, throughput requirements, and compliance pathway. Contact our engineering team to start the conversation.